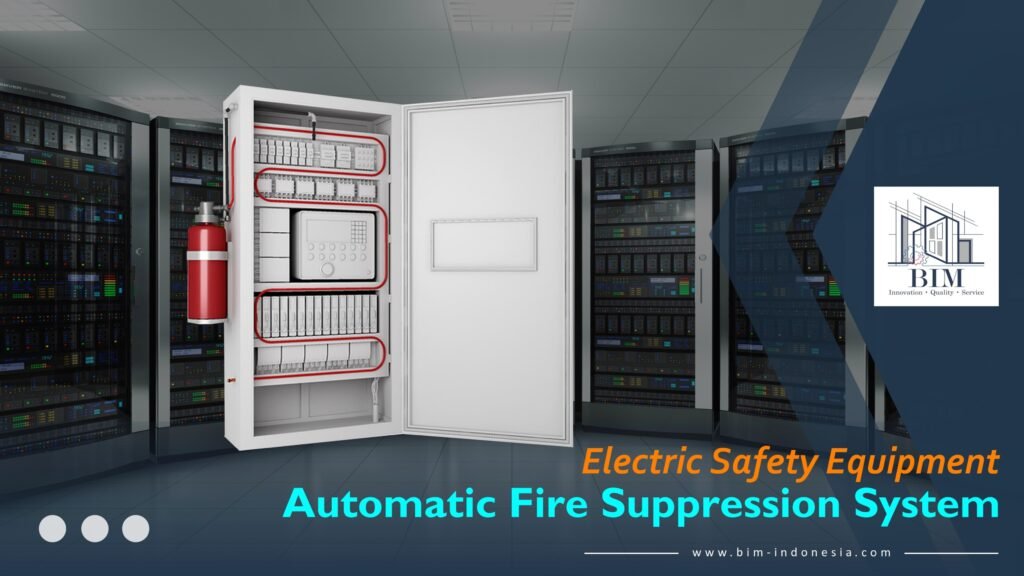
In many industries, valuable equipment operates nonstop in tough environments, making fire a major risk. BIM-Safety provides Automatic Fire Suppression Systems built to handle extreme conditions, ensuring continuous protection against fire damage.
Each system includes pressurized cylinders, valves, and nozzles that automatically release extinguishing agents when heat is detected — instantly controlling the fire and triggering an alarm.
Our systems deliver reliable protection for enclosed and high-risk areas, such as engine compartments and machinery spaces, across industries like construction, transportation, manufacturing, and energy.
BIM-SAFETY electric equipment fire suppression systems have been specifically designed to protect electric equipment and put out electric fires caused by leakage electric (class E fire) quickly and efficiently.
These self contained pneumatic systems require no external energy or power supply. Upon flame impingement or heat, the pressurized detection tubing will burst and activate the cylinder valve to open and release the extinguishing agent.
BIM-SAFETY electric equipment fire suppression systems are specifically designed to extinguish fires of electric panel, battery bay, control panel, electric equipment etc. It is developed to prevent damage of equipment, records, people and other assets that are vital to a business.
BIM-SAFETY ADVANTAGES :
⏱ Rapid fire detection and suppression
Automatically detects and suppresses fires within seconds, minimizing damage and downtime
🛑 Protect expensive equipment
Safeguards high-value assets such as excavators, dump trucks, drills, and shovels from fire-related losses
👷 Improve operator safety
It reduces the risk to human life by activating without manual input, even if the operator is unaware or unable to act
🕒 Reduce downtime
Prevent long-term operational shutdowns by extinguishing fires early, keeping machinery in service
📉 Lower insurance costs
Insurers often offer discounted premiums for equipment equipped with certified suppression systems
🌍 Suitable for harsh environments
Designed to function reliably in dusty, hot and vibrating conditions typical in mining operations
📋 Regulatory compliance
Helps meet safety regulations and standards (e.g., ISO, MSHA, NFPA)
♻️ Environmentally friendly agents
Uses cleaning agents (e.g., dry chemical, foam, novec) that are safe for electronics and the environment
🔧 Easy maintenance and monitoring
Many systems come with remote diagnostics and alerts, making maintenance and inspection efficient.
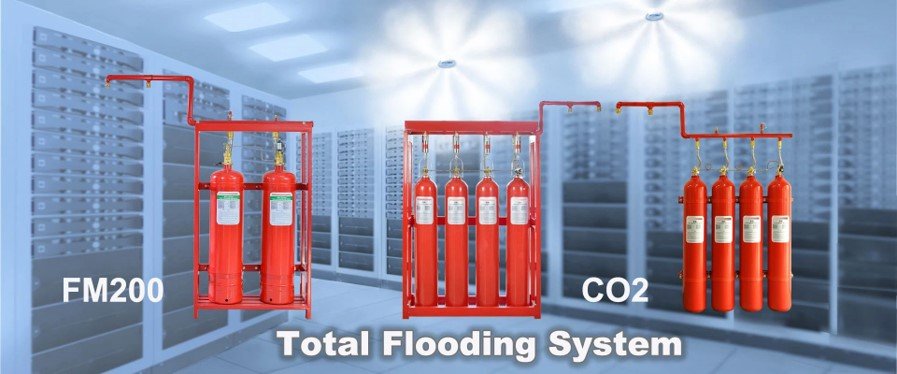
The FM200 HFC-227ea Fire system is widely used in various scenarios, including but not limited to :
Communication centers
Transformer and switch room
Control rooms
Test laboratories
Flammable liquid storage
Telephone exchange
Data processing centers
Chemical storage rooms
Libraries and museums
Critical military applications
Bank vaults
Libraries
Book stores
Electronic data processing
Computer rooms
Semiconductor manufacturing facilities
Industrial process control rooms
Petrochemical facilities
Operation Flow :
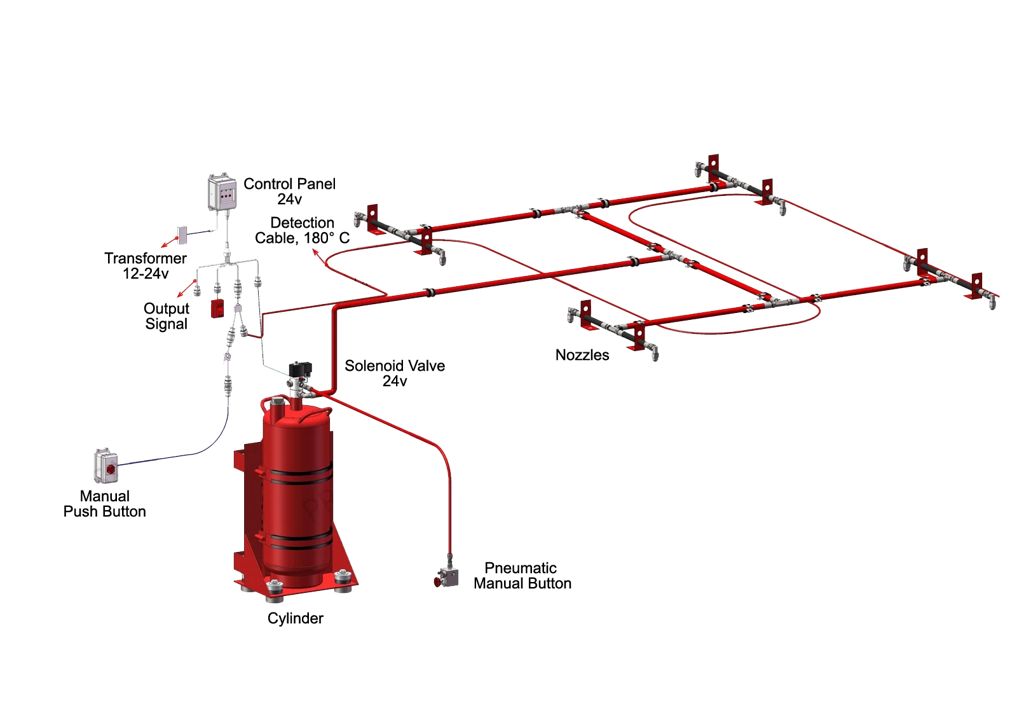
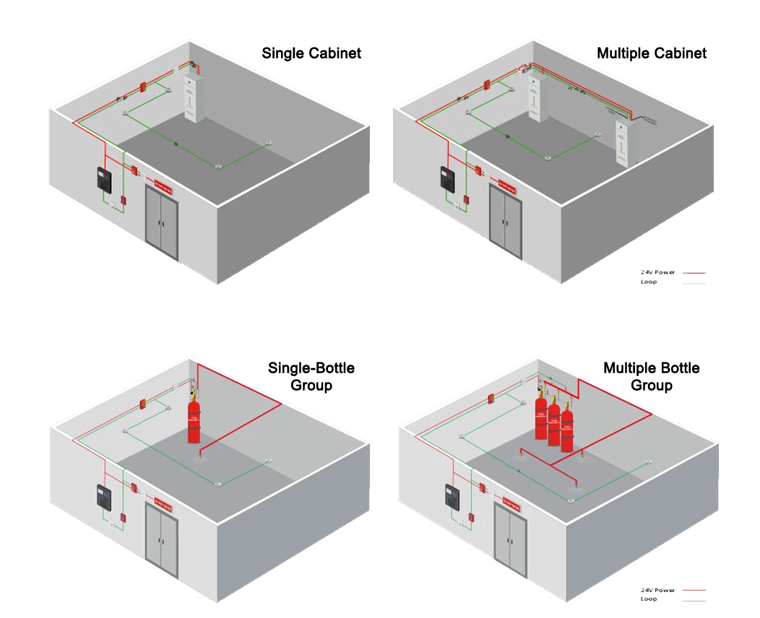
System Configuration :